A CNC machine creates value while it is machining, not while it waits for someone to exchange a part. Short idle intervals between cycles may look insignificant, yet they accumulate during breaks, shift transitions and periods when one operator is supporting other work. Automation can reduce those gaps, but only if the whole tending sequence is reliable enough to keep the spindle supplied rather than replacing brief waits with longer faults.
Measure the waiting time before designing the cell
The baseline should separate cutting time from manual loading, inspection stops, missing material, tool changes and unplanned alarms. This matters because a robot cannot recover every source of lost utilisation. A predictable three-minute machining cycle followed by a repeated manual exchange presents a different opportunity from a long unattended cycle where the operator already has time for other tasks. Product mix therefore matters more than a theoretical maximum schedule.
The tending cycle is an interface between systems
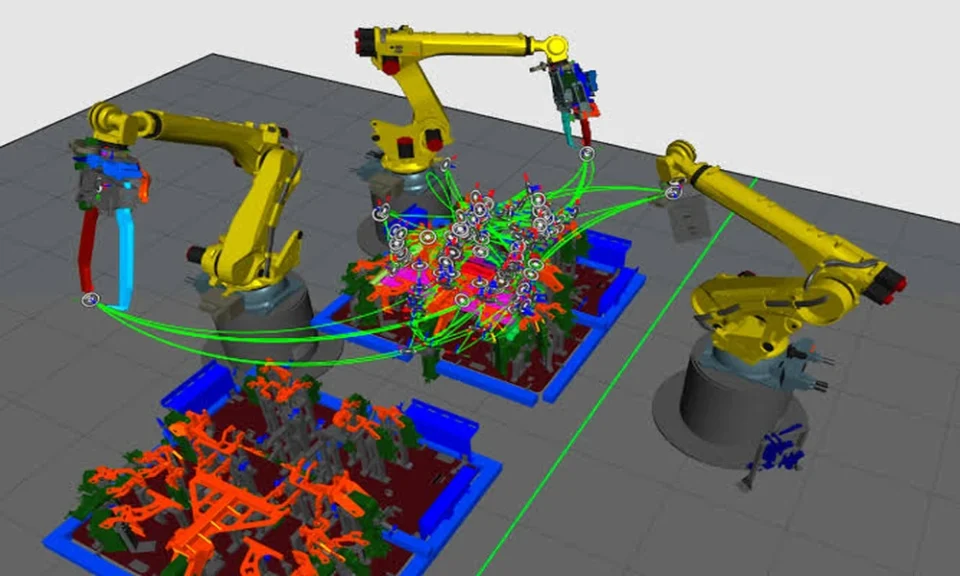
Reliable automation must coordinate part presentation, gripping, the machine door, fixture or chuck state, cycle-start signals and finished-part handling. The robot needs confirmation that it is safe and useful to enter the machine, and the cell must know whether a pickup actually succeeded. These interfaces are as important as the robot path because a perfectly timed motion sequence is worthless if the part is mis-seated or the machine is not ready.
Gripping and access decide how quickly the spindle restarts
Tool selection should be tested with the real surface condition of both raw and finished parts. In machine tending applications, coolant, chips, tolerance limits and centre of gravity can change grip stability or wrist dynamics compared with a clean demonstration sample. A dual-gripper arrangement may reduce machine idle time by carrying the incoming part while removing the finished one, but it also adds mass, size and collision constraints, so its benefit should be measured against a well-optimised single-tool cycle.
Buffers extend unattended operation
The cell can run only as long as it has raw material and space for finished parts. Trays, drawers, conveyors or feeders determine the unattended window, while their loading time remains human work that should be included in the labour estimate. Buffer design should also preserve traceability and surface protection. A useful setup allows replenishment to happen predictably without forcing the operator into awkward or unsafe interaction with the robot.
Exceptions determine effective utilisation
Missed grasps, chips in fixtures, worn tools and machine alarms are unavoidable over long operating periods. The cell should detect common failures before they create damaged tooling or suspect output, and alarms should state the process condition and authorised recovery. Teams should track intervention frequency and recovery duration because these values show where changes to presentation, gripping, cleaning or preventive maintenance will produce a larger utilisation gain than shaving seconds from normal motion.
More spindle hours must become good parts
Higher utilisation is valuable only when it produces conforming output that the business actually needs. Before-and-after comparison should include good-part count, scrap, rework, changeovers and planned downtime rather than only robot running hours. The strongest projects create a repeatable operating window in which buffers, maintenance, inspection and recovery all support longer productive machining. Under those conditions, skilled people can focus on decisions while the machine spends more of its available time cutting.
Utilisation should be treated as an operating metric
The benefit of tending automation can change with product mix, staffing patterns and maintenance condition, so the original business case should not be treated as permanent. Teams can periodically compare spindle waiting, intervention frequency, buffer shortages and good-part output to see whether the cell still removes the delays it was designed to address. That turns utilisation improvement into an ongoing operating discipline instead of a one-time commissioning claim.
